Double Wall Corrugated Boxes: Industrial Strength Shipping Solutions for Heavy Duty Packaging
By Marketing Team, OX BOX
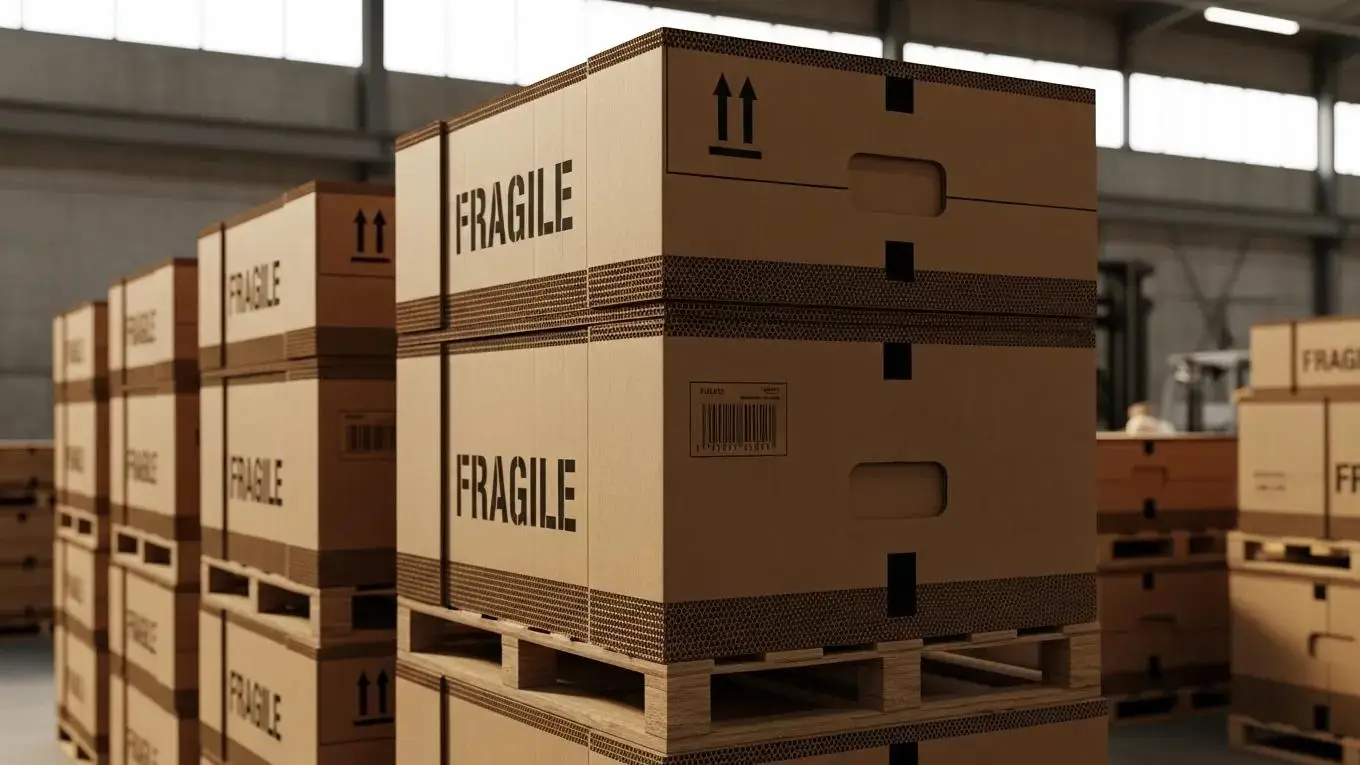
Double wall corrugated boxes are essential for businesses that require robust packaging solutions for shipping and storage. These boxes are designed to withstand significant weight and pressure, making them ideal for heavy-duty applications. In this article, we will explore the features, advantages, and applications of double wall corrugated boxes, as well as their material composition and construction methods. Understanding these aspects will help businesses make informed decisions about their packaging needs, ensuring that their products are protected during transit and storage. We will also discuss how companies like Ox Box provide specialized solutions for industrial-strength storage and shipping containers.
Double Wall Corrugated Boxes Overview
Double wall corrugated boxes consist of two layers of fluted paper sandwiched between three sheets of linerboard, providing enhanced strength and durability compared to single wall boxes. This construction allows them to handle heavier loads and offers better protection for fragile items. The design of double wall corrugated boxes makes them suitable for various applications, including shipping, storage, and retail display. Their versatility and strength make them a preferred choice for businesses looking for reliable packaging solutions.
Industrial Strength:
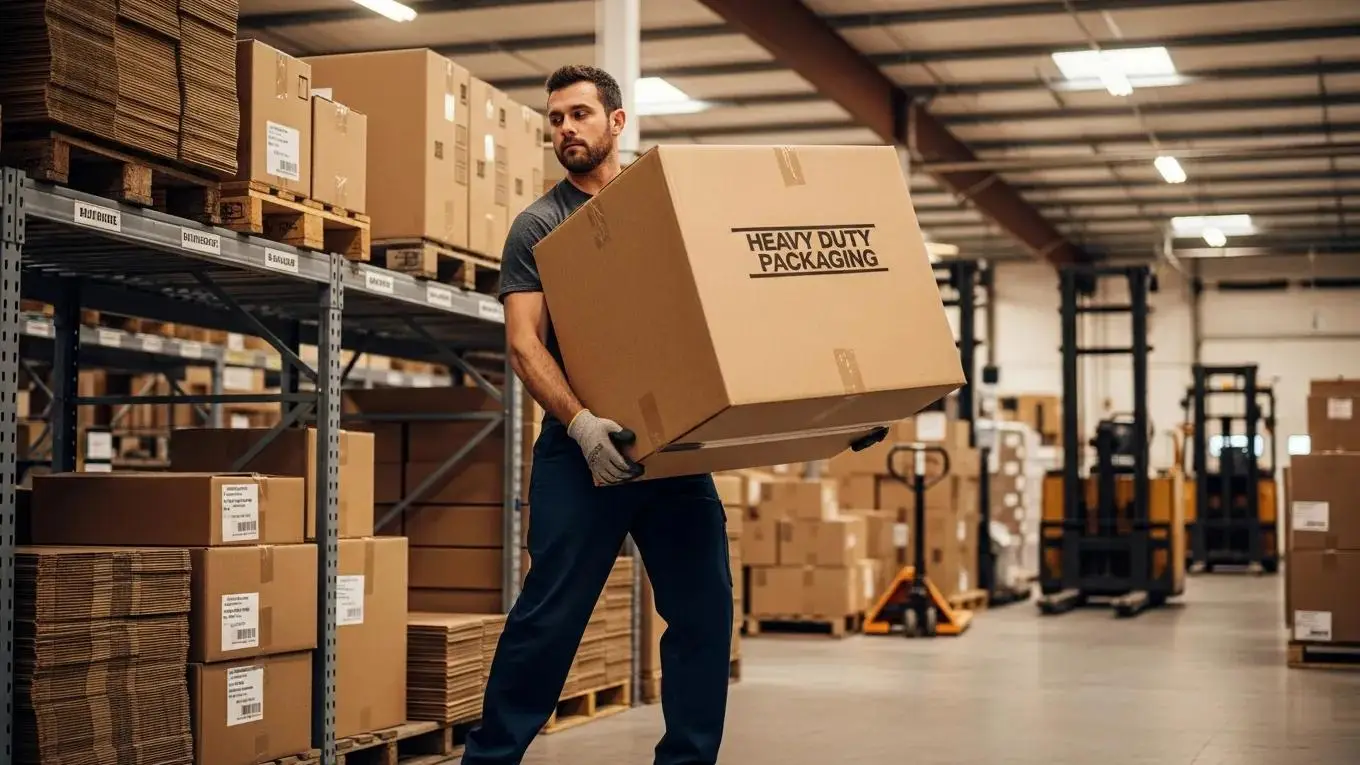
The industrial strength of double wall corrugated boxes is a key feature that sets them apart from standard packaging options. These boxes are engineered to provide superior protection against impacts, moisture, and other environmental factors. Their robust construction allows them to support significant weight, making them ideal for shipping heavy items. Additionally, double wall boxes are cost-effective, as they reduce the risk of damage during transit, ultimately saving businesses money on replacements and returns.
Applications for Heavy Duty Packaging:
Double wall corrugated boxes are widely used across various industries for heavy-duty packaging. Some common applications include:
- Shipping and Storage: Ideal for transporting heavy machinery, electronics, and other fragile items.
- Custom Solutions: Tailored designs to meet specific product dimensions and weight requirements.
- Industry Sectors: Used in manufacturing, retail, and logistics sectors for efficient packaging solutions.
These applications highlight the versatility and reliability of double wall corrugated boxes in meeting diverse packaging needs.
Advantages as Shipping Solutions:
Double wall corrugated boxes offer several advantages as shipping solutions, making them a popular choice for businesses:
- Strength and Durability: Their robust construction ensures that products remain safe during transit.
- Cost-Effectiveness: Reduces the likelihood of damage, minimizing replacement costs.
- Customization Options: Available in various sizes and designs to fit specific product requirements.
- Recyclability: Made from recyclable materials, contributing to sustainable packaging practices.
- Ease of Use: Lightweight yet strong, making them easy to handle and stack.
These benefits make double wall corrugated boxes an excellent investment for businesses looking to enhance their shipping processes.
Ox Box is a specialized provider of industrial-strength storage and shipping containers, focusing on durable packaging solutions for businesses. Their expertise in double wall corrugated boxes ensures that customers receive high-quality products tailored to their specific needs.
What Are Double Wall Corrugated Boxes and Their Material Composition?
Double wall corrugated boxes are made from layers of corrugated fiberboard, which consists of a fluted layer sandwiched between two linerboards. This construction provides the necessary strength and rigidity to support heavy loads. The materials used in these boxes are typically sourced from sustainable sources, ensuring that they are both durable and environmentally friendly. The combination of these materials results in a packaging solution that is not only strong but also lightweight, making it ideal for shipping.
How Is Double Wall Corrugated Board Constructed for Enhanced Durability?
The construction of double wall corrugated board involves several key processes that enhance its durability. First, the fluted paper is created by passing sheets of paper through a corrugating machine, which forms the characteristic waves. These flutes are then glued between two sheets of linerboard, creating a strong bond. The resulting structure is tested for strength and durability, ensuring that it meets industry standards for heavy-duty packaging. This meticulous construction process is what allows double wall corrugated boxes to withstand the rigors of shipping and storage.
What Are the Key Material Types Used in Heavy Duty Corrugated Boxes?
Heavy duty corrugated boxes utilize various types of materials to achieve their strength and durability. Key materials include:
- Corrugated Fiberboard: The primary material used, providing structural integrity.
- Linerboard: The outer layers that protect the contents and add strength.
- Fluted Paper: The inner layer that provides cushioning and support.
These materials work together to create a packaging solution that is both effective and reliable for heavy-duty applications.
What Is the Weight Capacity and Load Rating of 275 lb Double Wall Corrugated Boxes?
275 lb double wall corrugated boxes are designed to support a maximum weight of 275 pounds, making them suitable for heavy items. The weight capacity is determined by the box’s construction, including the type of materials used and the design of the flutes. This load rating ensures that the boxes can handle the demands of industrial shipping without compromising the safety of the contents.
How Do Weight Ratings Impact Industrial Shipping Container Performance?
Weight ratings play a crucial role in determining the performance of industrial shipping containers. A higher weight rating indicates that the container can support heavier loads without risk of failure. This is particularly important for businesses that ship heavy machinery or fragile items, as it ensures that the packaging can withstand the stresses of transportation. Understanding weight ratings helps businesses select the appropriate packaging for their specific needs, ensuring safe and efficient shipping.
What Testing Standards Verify the Strength of Double Wall Cardboard Containers?
Testing standards for double wall cardboard containers include various methods to assess their strength and durability. Common tests include:
- Edge Crush Test (ECT): Measures the compressive strength of the box.
- Bursting Test: Evaluates the box’s resistance to internal pressure.
- Drop Test: Assesses the box’s ability to protect contents during falls.
These testing standards ensure that double wall corrugated boxes meet industry requirements for strength and reliability, providing peace of mind for businesses.
Which Industrial Applications Benefit Most from Double Wall Corrugated Shipping Containers?
Several industrial applications benefit significantly from double wall corrugated shipping containers, including:
- Manufacturing: For shipping heavy machinery and components.
- Retail: For packaging products that require extra protection during transit.
- Logistics: For efficient storage and transportation of goods.
These applications demonstrate the versatility and effectiveness of double wall corrugated boxes in various sectors.
How Do Heavy Duty Corrugated Boxes Support Supply Chain and Storage Needs?
Heavy duty corrugated boxes play a vital role in supporting supply chain and storage needs. Their strength and durability ensure that products remain safe during transportation, reducing the risk of damage and loss. Additionally, these boxes can be easily stacked and stored, optimizing warehouse space. The customization options available also allow businesses to tailor their packaging to fit specific products, enhancing efficiency in the supply chain.
What Case Studies Demonstrate Ox Box Solutions in Demanding Environments?
Ox Box has successfully provided double wall corrugated solutions in various demanding environments. For instance, they have supplied packaging for the automotive industry, where heavy parts require robust protection during shipping. Their expertise in creating custom solutions has helped businesses streamline their packaging processes, ensuring that products arrive safely and on time. These case studies highlight the effectiveness of Ox Box’s offerings in meeting the unique challenges faced by different industries.
How Do Sustainability and Recycling Practices Enhance Double Wall Corrugated Box Use?
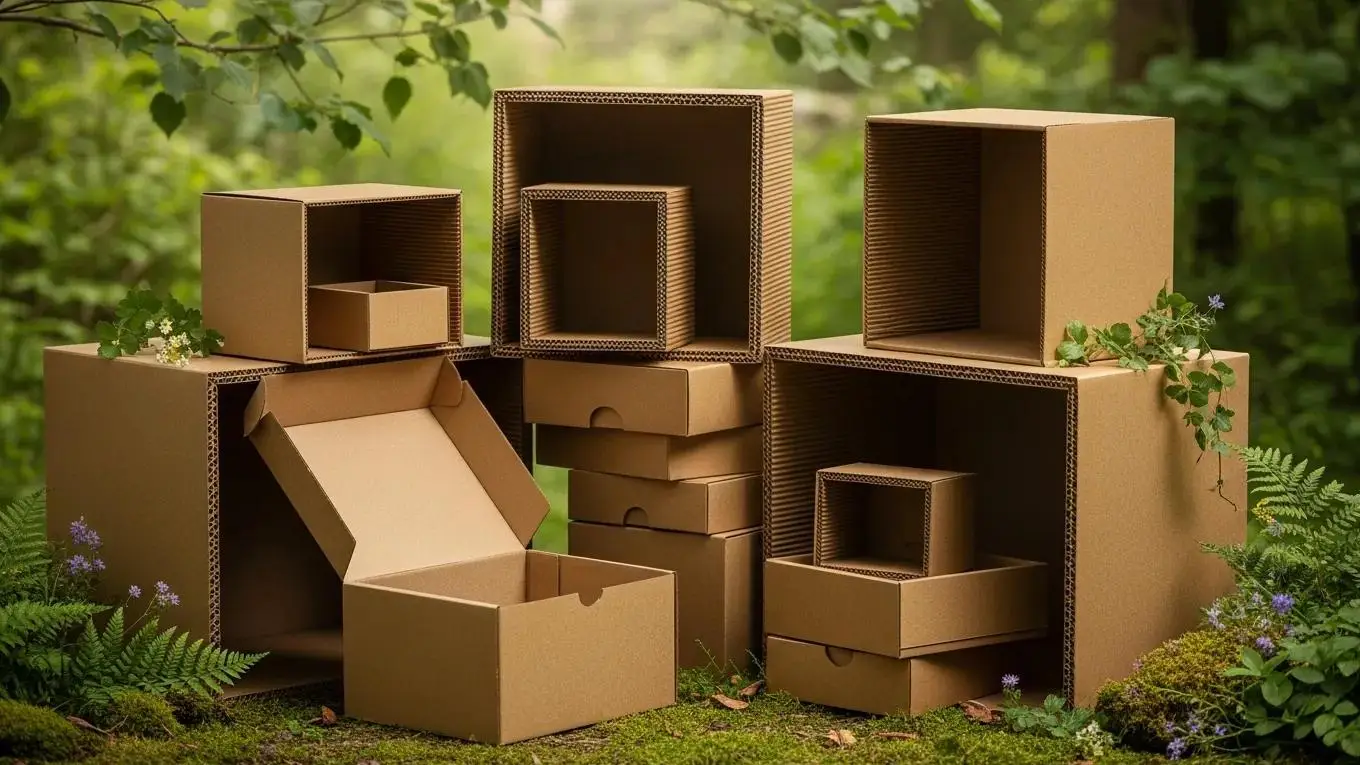
Sustainability and recycling practices are integral to the use of double wall corrugated boxes. These boxes are made from recyclable materials, which reduces waste and promotes environmental responsibility. Many businesses are now prioritizing sustainable packaging solutions, and double wall corrugated boxes fit this trend perfectly. By choosing recyclable packaging, companies can enhance their brand image and appeal to environmentally conscious consumers.
What Are the Environmental Benefits of Using Recyclable Corrugated Fiberboard Boxes?
Using recyclable corrugated fiberboard boxes offers several environmental benefits, including:
- Reduced Waste: Recyclable materials help minimize landfill contributions.
- Lower Carbon Footprint: Sustainable sourcing of materials reduces environmental impact.
- Conservation of Resources: Recycling conserves natural resources by reusing materials.
These benefits make recyclable corrugated fiberboard boxes an excellent choice for businesses looking to improve their sustainability practices.
How Does Ox Box Incorporate Eco-Friendly Materials in Industrial Strength Shipping Boxes?
Ox Box is committed to sustainability and incorporates eco-friendly materials in their industrial strength shipping boxes. They utilize recycled content in their packaging solutions, ensuring that their products are both durable and environmentally responsible. By prioritizing sustainable materials, Ox Box not only meets the demands of their customers but also contributes to a greener future for the packaging industry.